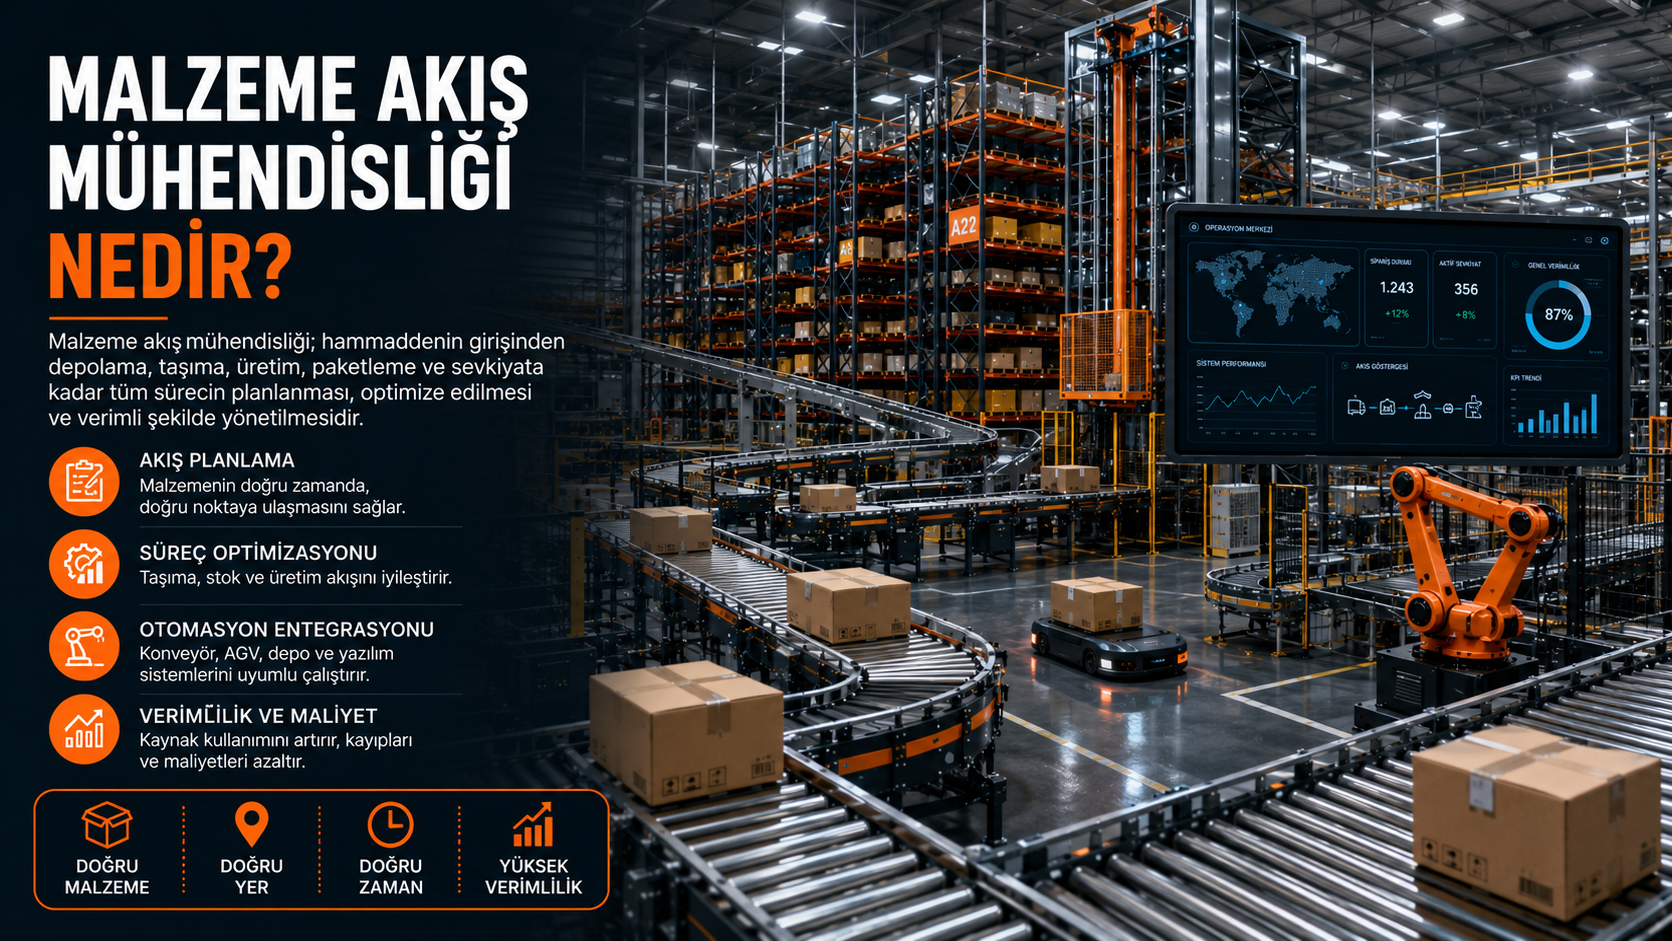
Material Flow Engineering is the engineering discipline that ensures the movement of products in the most accurate, safest and most efficient way in production facilities, logistics centers and warehouses. Today, due to increasing order volume, short delivery times and high operational expectations, businesses are turning to engineering solutions that plan the product flow holistically instead of investing only in equipment. Correctly applied Material Flow Engineering increases operational efficiency, reduces costs and gives businesses a sustainable competitive advantage. Material flow does not only refer to the transportation of products from one point to another. Product acceptance, storage, production feeding, order preparation, packaging and shipping processes are all within the scope of this engineering approach. Thanks to proper planning of the process, unnecessary transport movements are reduced, waiting times are reduced and operations become more controlled.
Why is Material Flow Engineering Important?
The operational structure of every business is different. Standard systems may not always be sufficient as product dimensions, order density, production model and warehouse capacity vary. Therefore, it is of great importance to develop business-specific solutions with the Material Flow Engineering approach.
- Product movements are optimized.
- Operation times are shortened.
- Human errors are reduced.
- Warehouse space is used more efficiently.
- Operation costs are reduced.
- Production and logistics processes are synchronized.
Continuous Product Flow with Conveyor Systems
In order to manage material flow efficiently, the right conveyor systems must be selected. Thanks to solutions appropriate to the product structure and operational needs, uninterrupted product flow can be ensured between production and warehouse.
Correct positioning of conveyor systems ensures that the products reach the target point without unnecessary waiting. Thus, while the operation speed increases, the need for labor decreases and the processes become safer.
Smart Product Routing with Sorter Technologies
In high-volume operations, directing products to the right point is one of the most critical stages of material flow. Therefore, correct planning of sorter systems is of great importance within the scope of Material Flow Engineering.
Thanks to sorter solutions, products are automatically directed to the correct line. This increases order accuracy, increases operational capacity and ensures faster shipping processes.
Efficient Material Flow with Smart Storage Systems
A successful Material Flow Engineering study does not only consist of conveying systems. It is also of great importance that the products are stored in the right locations, accessed as soon as possible when needed, and transferred to the production or shipping processes on time. Therefore, smart storage systems are among the indispensable components of modern material flow projects. Thanks to correctly planned automatic storage solutions, warehouse space is used more efficiently, product access times are shortened and stock accuracy increases significantly. Thus, businesses can respond faster to increasing order volumes.
Control of Processes with Software Integration
In modern Material Flow Engineering projects, software integration is as critical as mechanical systems. Thanks to the collaboration of WMS (Warehouse Management System), ERP and automation software, product movements are tracked in real time. This integration increases stock accuracy and provides operations managers with the opportunity to perform instant reporting and performance analysis. Thanks to real-time data management, bottleneck processes can be easily identified, product flow can be optimized and maintenance planning can be made more accurately. This ensures that operations continue uninterrupted.
Things to Consider in Material Flow Engineering Applications
Since the needs of each facility are different, engineering studies specific to the facility should be carried out instead of standard solutions. The correct automation infrastructure should be planned by analyzing product type, carrying capacity, daily order volume and growth targets.
- Detailed analysis of operational processes
- Choosing the right conveyor and sorter technologies
- Correct planning of storage systems
- Complete software integration
- Establishing infrastructure suitable for future capacity increase
Material Flow Engineering projects planned specifically for the business reduce operational costs and make production and logistics processes more efficient. Thanks to the right engineering approach, businesses can both meet their current needs and prepare for future growth targets with confidence.
You can contact us to get detailed information about material flow solutions and warehouse automation. Contact via WhatsApp For international information on material handling technologies: MHI – Material Handling Industry
Related guides: What is a conveyor? Types and selection guide · How is the conveyor system cost determined? · KOAL conveyor systems
Since 2010 we have designed, built, installed and serviced sorter and conveyor systems in Gebze. These articles draw on our field experience.