
Safe Vertical Transport Solutions with Case Pallet Elevators
Case pallet elevators are vertical transportation systems that enable the safe transportation of cases, pallets and product collection trolleys between floors in warehouses, production facilities, logistics centers and industrial enterprises. These systems are preferred to reduce time loss, risk of work accidents and operational disruptions caused by the transportation of heavy loads by human power.
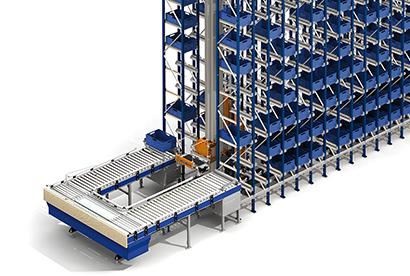
Thanks to the vertical elevator structure, plastic product crates, product collection trolleys and pallets can be automatically sorted, loaded and unloaded with accumulation conveyors. Thus, businesses save both time and labor.
Especially in businesses with heavy shipping, production and storage traffic, a correctly designed vertical transportation system makes the daily workflow more controlled and efficient. The ability to custom design dimensions according to customer needs makes the system a flexible solution for different sectors.
What are Case Pallet Elevators?
Case pallet elevators are automatic vertical transportation systems that enable the transportation of cases, pallets, product carts or similar loads between different floors or height levels. It enables the vertical transfer of products in areas where standard horizontal conveyor lines are insufficient.
These systems can work together with the production line, warehouse area, shipping point or accumulation conveyors. Once the loads enter the system, they are moved to the determined level and can be automatically transferred to the exit conveyor.
Case pallet elevators offer a safe, fast and orderly solution, especially in operations requiring heavy load transportation and product transfer between floors.
How Does the System Work?
Case pallet elevators work on the principle of taking the load from the entrance conveyor and moving it to the target height with vertical movement. The system transfers the product to the exit conveyor after the transportation process is completed.
When used with accumulation conveyors, products can be placed in a certain order and automatic loading and unloading operations can be carried out in a more controlled manner. This structure accelerates product flow, especially in multi-storey warehouses and production facilities.
Thanks to the braked motor structure, loads are transported safely. Elevator conveyor width, carrying capacity and maximum height can be specifically determined according to the project need.
Areas of Use
Case pallet elevators can be used in many industrial areas where vertical transportation is required. It is especially preferred in facilities where crates, pallets and product collection trolleys need to be transferred to different levels.
The main areas of use are:
- Warehouse and logistics centers
- Production facilities
- Shipment and goods acceptance areas
- Multi-storey warehouse systems
- Plastic case transport lines
- Palletized load transport systems
- Product collection trolley transfer lines
- Systems with accumulation conveyor connection
- Industrial automation lines
- Food, pharmaceutical, packaging and production facilities
The vertical transportation system used in these areas allows products to move faster, safer and more regularly between floors.

For Which Loads Are Case Pallet Elevators Suitable?
These systems can be designed according to different load types. The weight, size, base structure and intended use of the load to be carried directly affect the system design.
Suitable load groups are:
- Plastic product crates
- pallet loads
- Product collection carts
- Boxed and boxed products
- In-warehouse handling equipment
- Production line intermediate products
- Product groups ready for shipment
- Loads to be taken to the accumulation line
Custom design of dimensions according to customer needs provides the advantage of adapting to different operations for case pallet elevators.
Advantages of Case Pallet Elevators
Case pallet elevators do not only offer vertical transportation convenience to businesses. It also provides significant benefits in terms of time saving, occupational safety, automation compatibility and operational efficiency.
Saves Time
Manual methods may cause loss of time in inter-floor transportation. Thanks to the automatic vertical transport system, loads are transferred to the target point faster.
This speeds up the workflow, especially in intensive production and shipping processes.
Reduces Labor Need
Manually moving heavy cases, pallets or product carts can be tiring and risky for workers. The system reduces manual workload by automating these transport operations.
Thus, employees can be assigned to more productive areas.
Provides Safe Transportation
The braked motor structure and controlled vertical movement system help carry loads safely. This structure reduces the risk of work accidents and increases operational safety.
Safe system design is of great importance, especially in heavy load transportation processes.
Offers Automatic Loading and Unloading Opportunity
When used with accumulation conveyors, loads can be automatically sorted, taken to the elevator and unloaded to the exit point.
This feature creates a more orderly product flow in warehouses and production lines.
Can be designed specifically for the project
Case pallet elevators can be produced in special sizes according to customer needs. Technical details such as carrying capacity, conveyor width, maximum height and speed can be determined according to the project.
In this way, the system can be adapted to the current operational structure of the business.
Technical Information: 1000 kg Capacity System
| Feature | Value |
|---|---|
| Maximum Load | 1000kg |
| Engine Type | engine with brake |
| Voltage Type | 400V |
| Maximum Engine Power | 8 kW |
| Elevator Conveyor Width | 420 / 620 / 820mm |
| Maximum Height | 12000 – 18000mm |
| Feed and Output Conveyor Speed | 0.3m/sec |
| Ambient Temperature | 0 ºC – 45 ºC |
Technical Information: 200 kg Capacity System
| Feature | Value |
|---|---|
| Maximum Load | 200kg |
| Engine Type | engine with brake |
| Elevator Conveyor Width | 420 / 620 / 820mm |
| Maximum Height | 12000 – 18000mm |
| Maximum Speed | 2m/sec |
| Ambient Temperature | 0 ºC – 45 ºC |
What to Consider When Choosing a System?
When choosing case pallet elevators, not only the load capacity but also the facility structure and operation need should be evaluated together. Correct project planning is critical for the efficient and safe operation of the system.
Load Capacity
The maximum weight of the products to be transported must be calculated correctly. While systems with a capacity of 1000 kg may be preferred for palletized loads, solutions with a capacity of 200 kg can be considered for lighter case and product trolley applications.
Transport Height
The maximum height can be planned between 12000 – 18000 mm. The correct height should be determined by taking into account the floor height, shelving system and exit point.
Conveyor Width
Elevator conveyor width can be evaluated with 420, 620 and 820 mm options. The appropriate width should be selected according to the size of the crate, pallet or product cart to be transported.
Need for Speed
The infeed and exit conveyor speed or maximum conveying speed should be determined according to the intensity of the operation. In businesses with intense product flow, speed planning must be done correctly.
Integration Structure
The system must work in harmony with accumulation conveyors, input-output lines, production line or warehouse automation structure. Correct integration ensures uninterrupted product flow.
Benefits to Businesses
Case pallet elevators provide businesses with many operational advantages in vertical transportation processes.
The main benefits are:
- Reduces load carrying time between floors
- Reduces labor requirement
- Enables safe transportation of heavy loads
- Offers automatic loading and unloading
- Can work integrated with accumulation conveyors
- Provides regular product flow in warehouse and production areas
- Reduces the risk of work accidents
- Can be specially designed for different load types
- Offers high carrying capacity
- Increases operational efficiency
These benefits make the system a powerful vertical transport solution, especially in multi-storey facilities and businesses with heavy product traffic.
Maintenance and Long-Term Use
Regular maintenance is required for case pallet elevator systems to operate safely and efficiently. The engine, brake system, conveyor surface, carrier structure and electrical connections should be checked periodically.
Things to consider during the maintenance process:
- Brake motor should be checked regularly
- The elevator carrier mechanism should be examined
- Input and output conveyors should be checked
- Electrical connections should be checked
- Conveyor surface must be kept clean
- Load sensors and safety equipment should be tested
- Moving parts should be checked periodically
- Operators should be trained in correct use
Regular maintenance maintains system performance and prevents unplanned downtime.
Technical Support and Communication
You can contact our expert team to get detailed information about case pallet elevators, evaluate the technical specifications according to your project, or determine the vertical transportation system suitable for your business.
A special solution can be developed for your project according to product type, load capacity, maximum height, conveyor width, entry-exit conveyor structure and automation needs.
For detailed information, you can contact us via our contact page.